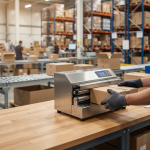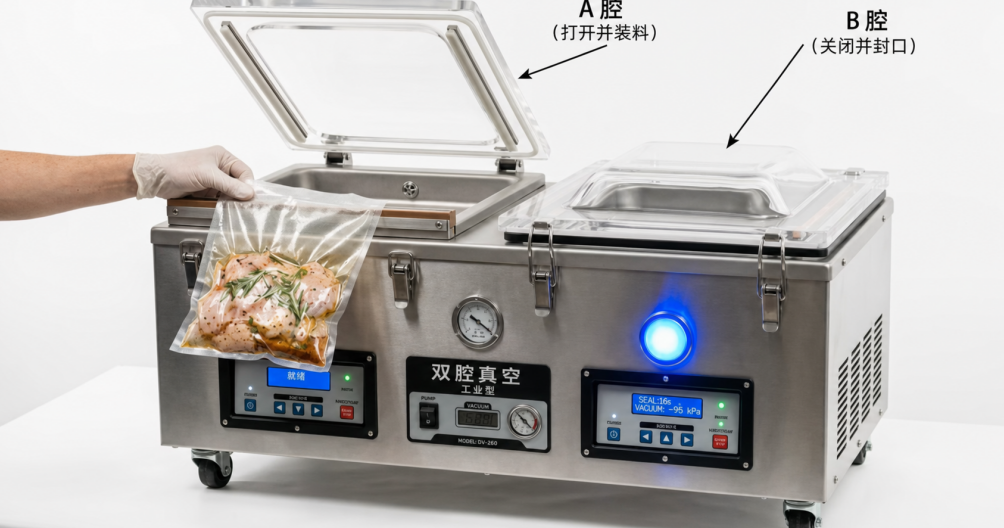
A dual-chamber vacuum packaging machine (also known as a twin-chamber vacuum packaging machine) is equipped with two independent vacuum chambers that share a single vacuum pump and control system. While one chamber is undergoing the vacuuming and sealing process, the operator can load products into the other chamber for packaging. The machine alternates between the two chambers in a continuous cycle, significantly improving production efficiency.
Dual-chamber models redefine production capacity advantages:
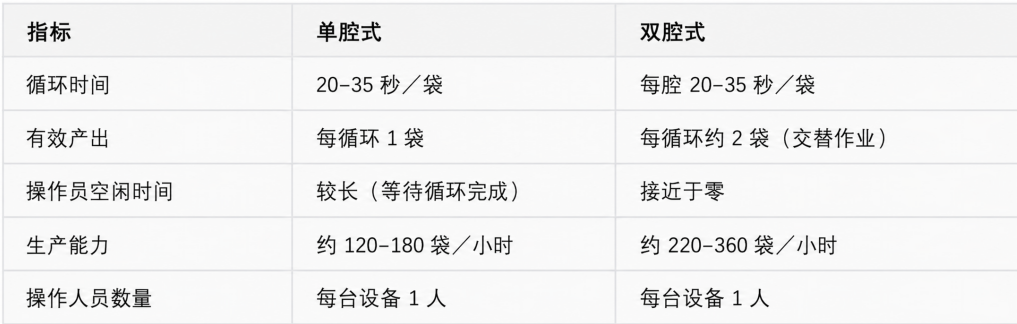
Scenarios where dual-chamber vacuum packaging machines are suitable:
Production capacity requirements consistently exceed 200 bags per hour
Prioritize reducing labor costs (single-person operation, doubled production capacity)
When processing high-value products, the intervals between vacuum pump operations can result in significant losses.
It can process two different product sizes simultaneously (each cavity corresponds to one product).
Situations where a single-chamber model is still appropriate:
Production capacity is less than 150 bags per hour
The factory building has limited floor space
Budget constraints (the two-room model is more expensive than the 40%–80%)
YGPACK Dual-Chamber Series: The DZ-500/2SB and DZ-600/2S series feature independently programmable chamber parameters, allowing different vacuum levels and sealing times to be set for each chamber. This makes them ideal for packaging products in bags of varying thicknesses on the same production line.